Related Topics:
Explosion Proof Pipe Inspection-
Secondary status inspection of relay protection
Secondary injection checks the operation of the protective system but does not check the primary circuit of the current transformer. The new generation of intelligent substations has achieved online monitoring functions for secondary equipment, making some state variables of relay protection equipment become observable indicators. These are not repeated unless incorrect operation occurs. Most frequently they are performed by simulating test conditions by means of portable test sets. Other methods include : tests using. This guide explores the different types of protection relays and their testing procedures, with a focus on tools like secondary injection test sets and three-phase relay test sets. For over 50 years, Electrical Reliability Services (ERS) has been providing startup.
[PDF Version]
-
Fiber Optic Cable Sheath Inspection Section
The procedures in this document describe basic inspection techniques and processes of cleaning for fiber optic cables, bulkheads, and adapters used in fiber optic connections. These types are (Figure 1): Type A 1) The sheath is peeled or chipped. 2) No portion of the armor or cable core is exposed. After cable placement is complete the residual tension on the cable should be less than this value. NOTE: Steps that reference. There are three main principles that needs to be taken in consideration for an efficient optical connection: a perfect core alignment, perfect physical contact and dirt-free connectors.
[PDF Version]
-
Principle of Automatic Visual Inspection of Fiber Optic Patch Cords
Endface inspection focuses on the visible quality of the polished fiber surface and surrounding ferrule area. You use a fiber microscope or automated inspection scope to check for contamination, pits, chips, cracks, and scratches. Even a small dust particle or scratch on the endface can increase insertion loss, reduce return loss, and introduce random link instability. The primary reason for fiber inspection is to ensure that the connectors are free of any defects, damage, or debris that would prevent sufficient transmission of light when mated. Normal Inspection Items for Fiber Optic Patch Cords Fiber optic patch cords are critical components in communication systems, connecting various devices and ensuring efficient data transmission. To maintain high-quality performance, a thorough inspection process is essential. The. FOCIS WiFi2 is an ergonomic Fiber Optic Connector Inspection System that, when paired with an iOS or Android smart device, provides fast and accurate IEC/IPC/AT&T compliant and user-defined pass/fail end-face cleanliness analysis. FOCIS Duel is a self-contained twin-ported Bluetooth connected fiber.
[PDF Version]
-
Relay Protection Inspection Procedures
During visual inspection, the relay should be checked for any signs of damage, such as physical wear and tear, loose connections, or corrosion. These devices spend years in standby mode, waiting to isolate faults in milliseconds when called upon. Yet without structured, documented maintenance, organizations often discover relay. The testing and verification of relay protection devices can be divided into four groups: Type tests are needed to prove that a protection relay meets the claimed specification and follows all relevant standards. Since the basic function of a protection relay is to correctly function under abnormal. Protective circuit functional testing, including lockout relay testing, must take place immediately upon installation, every 2 years thereafter, and upon any change in wiring. Acceptance tests fall into two categories : (i) On new relays which are to be used for the first time. Applications: Overcurrent. THEY SHOULD BE GIVEN FIRST LINE MAINTENANCE ATTENTION. ” relay may only need to operate for 0.
[PDF Version]
-
Inspection Regulations for Small Busbars
IEC 61439 is a standard developed by the International Electrotechnical Commission (IEC) that covers design verification for low-voltage electrical products and assemblies. RoHS-compliant busbars are widely used in telecom and industrial electrical systems. Quality busbars typically undergo multiple inspections, including: These tests ensure compliance. The purpose of this method is to verify the functionalities of a Metal Enclosed Busb ar. This. ULTRUS™ helps companies work smarter and win more with powerful software to manage regulatory, supply chain and sustainability challenges. Award-winning software and advisory services for ESG management and. Are you aware that improper installation of busbars can lead to costly and dangerous electrical failures? This article details the comprehensive standards for installing and inspecting busbars, including support brackets, insulators, and bus duct systems.
[PDF Version]
-
Sample Inspection Report for Metal Distribution Boxes
This is a sample inspection report template. For every product inspection service, our technical team meticulously prepares a detailed inspection checklist, tailored to your specifications and the general inspection standard ANSI/ASQC Z1. It does not relieve the manufacturers from their contractual obligations nor prejudice client's right for compensation for any apparent and/or hidden defects not detected during our b xes, not e ss er is listed hereAn Inspection Report Template is a standardized document used by inspectors across various industries to record findings from an inspection process. It outlines a comprehensive checklist of criteria, benchmarks, and observations necessary to assess conditions, compliance with regulations, or. A material receiving inspection report enables material controllers to document the inspection and verification of incoming construction materials. A well-documented material. Ensure your materials meet the highest standards with the Material Quality Inspection Report Template, offered by Template. R: Document Review = Review means Review document, which includes of material test.
[PDF Version]
-
Fiber Optic Switching Zone
It discusses what zoning is, why it is needed for access control and isolation, how zoning works through configuration and activation of zone sets and zones, and best practices for connecting switches and ensuring consistency. Key terms like zone set . “The Fibre Channel Industry Association (FCIA) is a mutual benefit, non-profit, international organization of manufacturers, system integrators, developers, vendors, and industry professionals, and end users. Zoning a fibre channel network at the switch level provides a security boundary that ensures host devices do not see. This entry describes the various possible combinations and necessary properties of devices, cables, etc. that are used for an optical PROFINET connection in hazardous areas, in particular to an ET200iSP station or similarly suitable peripheral stations in explosion protection zones 1 or 21. Each zone defines the set of Fibre Channel initiators and Fibre Channel targets that can communicate with each other in a VSAN. Similar to the VLAN function of an Ethernet switch, the zoning function of a Fibre Channel.
[PDF Version]
-
Relay Protection Inspection and Maintenance
Relay maintenance generally consists of : Inspection and burnishing of contacts. Adjustments checking (iv) Breakers tripped by manual contact closing. Most frequently they are performed by simulating test. Protective circuit functional testing, including lockout relay testing, must take place immediately upon installation, every 2 years thereafter, and upon any change in wiring. Protective relays are your most powerful defense against long, costly outages and extensive. Servicing protective relays per manufacturer and NETA recommendations ensures they work properly to prevent injury or extensive damage to your plant during an electrical distribution abnormality. To properly test relays, understanding their classification by design and application is essential. This. In the rapidly evolving industrial landscape of Electrical Equipment Manufacturing, the role of an Electrical Maintenance Engineer is more critical than ever. This article delves deep into.
[PDF Version]
-
Grounding of optical cable protection pipe
Follow these steps at each cable entry point and termination location to achieve a compliant, safe ground bond: Identify metallic components. Visually identify armor, strength. This Applications Engineering Note (AE Note) discusses conventional bonding and grounding practices for conductive fiber optic cable and hardware installations within the scope of the National Electrical Code (NEC). Nowadays, many electrical circuit components, apart from electronic devices, are microprocessor-based and sensitive to electromagnetic disturbances. Lightning is an electrical discharge within clouds either from cloud to cloud or from cloud to the earth. It has great impacts on communication stations and other signal circuits. Since the lightning. Fiber optic cable transmits data as light through glass or plastic strands, which means the fiber core itself carries no electrical current and requires no grounding. Either rigid or flexible, made of PE, PP or PVC, sand-proof, waterproof or fireproof.
[PDF Version]
-
Standards for Cable Tray and Pipe Gallery Supports
The International Electrotechnical Commission (IEC) provides detailed guidelines for cable tray systems under IEC 61537. This standard outlines the construction requirements, testing methods, and performance parameters for cable trays and related support systems. For proper installation, design, and maintenance, adherence to international standards is essential. One of the most recognized frameworks globally is the IEC standard for. OBO BETTERMANN has offered prod-ucts and solutions for electrical instal-lation for over 100 years. The Cable Tray ng standards, performance standards, test standards and application in this document have been tested extens ompetent professional en completely installed, without damage either to conductors or. Cable tray (or cable ladder) systems are a popular alternative to electrical conduit systems, as they have an outstanding record for dependable service, design flexibility and cost savings in commercial and industrial applications.
[PDF Version]
-
Inspection of wiring in fire protection electrical cable trays
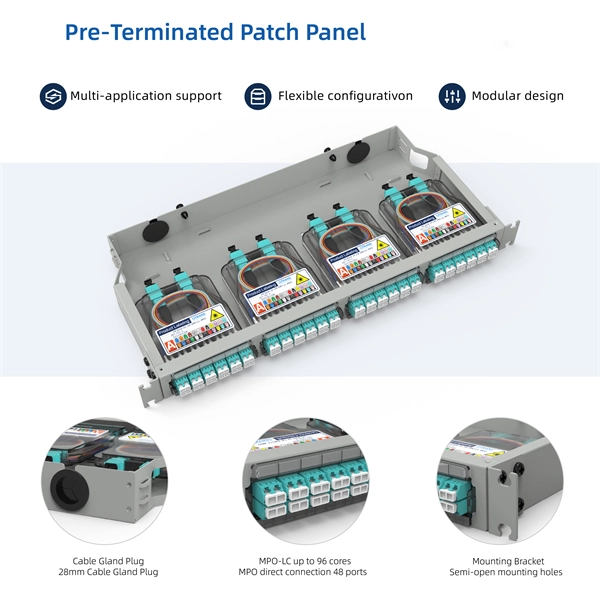
Inspect tray covers for proper installation to protect against dust, water ingress, and mechanical impact. Confirm covers in hazardous or outdoor areas meet relevant IP ratings. Check for smooth transitions at tray bends using factory-fitted components to prevent cable . Regular inspection of fireproof cable tray covers is essential for maintaining electrical system safety and fire protection integrity. The process described here takes a systematic approach to ensuring that cable tray installations meet safety, reliability, and project-specific needs while following to. Scope: Firestopping for busway, cable trays, cables, and trunking passing through walls in enclosed electrical installations. Where cables pass through shafts, walls, slabs, or enter electrical panels or cabinets, openings shall be tightly sealed with firestopping materials in accordance with.
[PDF Version]
-
Reserved length for optical cable in jacking pipe
Corning Optical Communications field trials have confirmed that a single air-assisted device can install 1500 to 2100 meters (5000 to 7000 feet) of optical fiber cable under good conditions. Longer lengths can be achieved by cascading devices (i., providing mid-assist). nts of any drive with economics being a key factor. Pit sizes will vary according to the excavation methods employed, although these ructed to provide a reaction against which to jack. 250-300mm at the bottom is sufficient. In places where underground pipes, electric main etc. come in the way trenches deeper than one meter shall be dug as necessary and DWC pipes shall be placed to protect the. The sub-hole tube should expose about 15cm of the remaining length of the tube hole in the hand hole. The interface between the sub-pipe in the hand hole and the plastic textile network pipe is wrapped with PVC tape to prevent the infiltration of sand. For loose tube and ribbon cable, the bend radius is specified at 20 times the cable diameter during tension/installation conditions and 10 times during static conditions (check the data sheet).
[PDF Version]